
Ražošanas process
Pilates Reformer Manufacturing Process: 12 Steps from Steel to Studio
A reformer is a machine of simple parts and demanding tolerances. This page follows the 12-step journey every Megacore reformer takes, from the first CAD drawing to the container at the loading dock. Each stage has its own quality checkpoint, so problems are caught where they happen rather than at the end of a run. Buyers who understand this flow can ask sharper questions, read our test reports with confidence and plan realistic launch dates. Between the steps you will also find where materials are inspected, how frames are welded and coated, how springs are matched for consistent feel, and how every finished unit is tested before it ships.
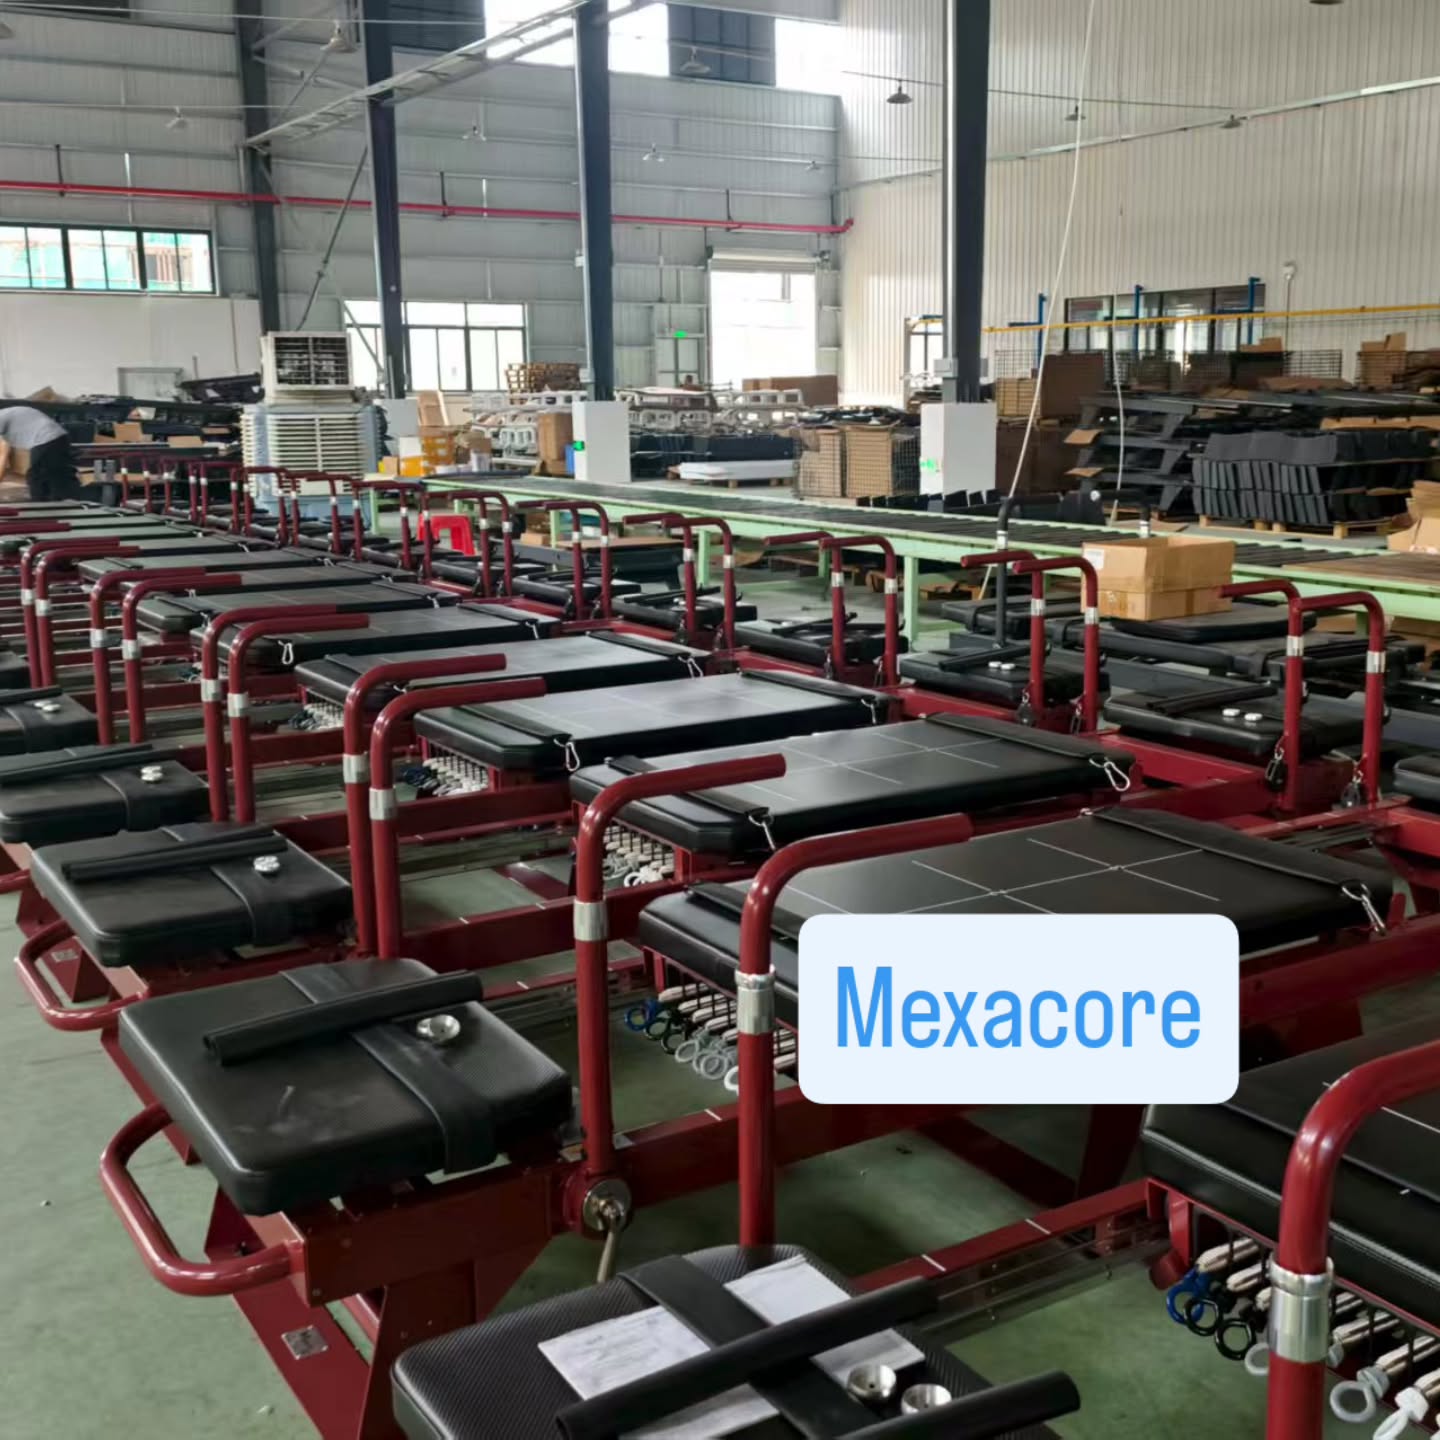
Step 01 - Design and Engineering
Every model starts as a CAD drawing built around load specifications, ergonomics and commercial-use expectations. For OEM projects our engineers review your design for manufacturability and structural safety before any metal is cut.
Getting the drawing right at this stage costs far less than reworking tooling later, and it fixes the frame geometry that everything downstream depends on.
- Checkpoint: drawing review and load-specification sign-off
Step 02 - Material Sourcing and Incoming Inspection
Steel tubes, aluminum profiles, springs, foam and vinyl are sourced from vetted suppliers. Every batch is checked on arrival for grade, dimensions and surface quality before it enters the warehouse.
Substandard material never reaches the production floor, which is what allows consistent output across large batches.
- Checkpoint: incoming material inspection record
Step 03 - Cutting and Forming
CNC cutting and tube bending shape raw material into frame components against drawing tolerances. Consistent geometry at this stage is what makes every reformer in a batch feel identical on the studio floor.
- Checkpoint: dimensional verification against CAD
Step 04 - Frame Welding
Frames are welded in precision jigs so alignment stays consistent from unit to unit. Weld strength is the backbone of structural safety, because a commercial reformer carries heavy load and thousands of repetitions a year.
- Checkpoint: weld integrity and alignment inspection
Step 05 - Grinding and Polishing
All surfaces are ground and polished to remove sharp edges, burrs and weld spatter. This protects users and staff from skin contact with rough metal and prepares the surface for a clean finish.
- Checkpoint: edge and surface smoothness check
Step 06 - Anti-Rust and Surface Treatment
Components receive anti-rust treatment so the frame stays protected even before final coating. This matters for machines that travel by sea in humid containers.
- Checkpoint: treatment coverage inspection
Step 07 - Electrostatic Powder Coating
Powder coating is applied electrostatically and cured in an oven, producing a scratch- and moisture-resistant finish that holds up to daily cleaning and years of studio use.
- Checkpoint: coating thickness and adhesion test
Step 08 - Upholstery and Padding
Foam is cut to density specifications and covered with commercial-grade vinyl by experienced upholsterers. Seam placement and stitch tension are controlled because padding takes the heaviest daily abuse.
- Checkpoint: stitching and seam strength check
Step 09 - Spring, Rope and Pulley Fitting
Springs are matched to resistance specifications and fitted with ropes and pulleys. Spring tension consistency is what gives a studio the same feel across all of its reformers.
- Checkpoint: spring calibration and tension matching
Step 10 - Final Assembly
Apmācīti montētāji saliek ratiņus, atdures, siksnas un furnitūru. Skrūves tiek pievilktas atbilstoši specifikācijai, un katra kustīgā daļa tiek noregulēta vienmērīgai kustībai pa visu sliežu garumu.
- Checkpoint: hardware torque and travel check
Step 11 - Testing and Adjustment
Each finished unit is load-tested, balanced and checked for smooth glide, quiet operation and firm stopper engagement. This is the same 12-point final inspection described on our quality control page.
- Checkpoint: full 12-point final inspection
Step 12 - Cleaning, Packing and Staging
Machines are cleaned, wrapped and packed with protective materials, then staged for container loading. Export packaging standards are covered in detail on our packaging and shipping page.
- Checkpoint: packing completeness and loading plan
Kvalitātes kontroles punkti īsumā
Quality is checked at every stage rather than only at the end. The table below summarizes what is verified and why it matters to the studio that eventually owns the machine.
Posms
Kas tiek pārbaudīts
Kāpēc tas svarīgi jūsu studijai
Materiāli
Marka, izmēri, virsmas kvalitāte
Novērš vājus rāmjus un priekšlaicīgu nolietošanos
Cutting and welding
Tolerances, metinājumu integritāte, izlīdzinājums
Konstrukcijas drošība lielas komerciālās slodzes apstākļos
Pārklājums
Biezums, saķere, pārklājuma vienmērība
Apdare, kas iztur gadu ilgu tīrīšanu
Polsterējums
Šuvju stiprums, putu blīvums
Padding that does not flatten after months of classes
Atsperes
Kalibrēšana, sprieguma konsekvence
Identical feel across every reformer
Gala vienība
Slodze, slīdēšana, balanss, drošība
Katra iekārta pārbaudīta pirms nosūtīšanas
Ražošanas laika grafiks
Lead times depend on the model, quantity and level of customization. We confirm exact dates in your production schedule after ordering and share milestone photos and videos so you can track progress.
Posms
Parastais ilgums
Ko jūs saņemat
Parauga ražošana
Typically 15-25 days
Viena pilnībā testēta vienība apstiprināšanai
Sērijveida ražošana
Typically 25-40 days
Milestone photos and videos, batch testing report
Jūras kravu pārvadājumi
Varies by route
Izsekošana, pārvadājumu dokumenti, atbalsts ierašanās brīdī
Kā izsekot savu pasūtījumu ražošanas laikā
Jums nav jāgaida piegāde, lai uzzinātu, kā sokas jūsu pasūtījums. Kad partija ir nodota ražošanai, mēs sniedzam atjauninājumus noteiktos posmos un atbildam uz jautājumiem, kamēr vēl ir laiks kaut ko pielāgot.
If you want a closer look, we can open a live call at the station of your choice, whether that is welding, coating, assembly or final testing.
- Kickoff confirmation - model, quantity, configuration and schedule locked before material release
- Material release update - your batch enters the line with a reference number
- Mid-production update - photos and video from welding and coating stages
- Assembly and testing update - units built, springs matched and inspections logged
- Packing and loading update - crated units, loading photos and shipping documents
- Arrival support - tracking shared through transit and help at your destination port or door
Kas var noiet greizi un kā mēs to novēršam
Two things decide whether a batch holds up: the drawing is checked against real load conditions, and no component changes between sample and bulk. Both are controlled as part of our process.
Our answer is fixed checkpoints, matched components and the same inspection standard for the sample and the volume run. Where a specification is unusual, we test and document it before committing to a full batch.
- Rasējumi pārbaudīti slodzes un ražošanas iespējamības ziņā pirms instrumentu izgatavošanas
- Atsperes un furnitūra visā partijā saskaņotas pēc vienas specifikācijas
- Starpposma pārbaudes noteiktos intervālos, nevis tikai partijas beigās
- Partiju uzskaite ļauj jebkuru vienību izsekot līdz tās pārbaudei
Biežāk uzdotie jautājumi
Samples typically take 15-25 days including finishing, and bulk production usually runs 25-40 days depending on quantity and customization, plus sea freight to your port. Exact dates are confirmed in your production schedule after ordering, and we flag any change as soon as it is known.
Yes. We send production photos and videos at milestone stages, including frame welding, coating, assembly and packing. You can also join a live video call to watch your line in real time if you want a closer look at any station.
Studio clients notice when reformer number one feels different from reformer number twelve. Spring calibration, welding jigs and standardized assembly are what keep every unit in a batch performing identically, so a class experiences the same resistance on every machine.
A unit that fails any checkpoint is pulled from the line and corrected before it can move forward. In-process checks catch most issues at the station where they happen, so a defect is not repeated across a whole run. Final inspection must be signed off before packing and loading.
Runāt ar mūsu inženieri
Tell us your model, quantity and target market. We’ll reply with pricing, lead time and sample options.